Product-specific
pH, water activity, formulation, viscosity, particles, heat penetration and target microorganisms influence the required process.
Evidence / process safety
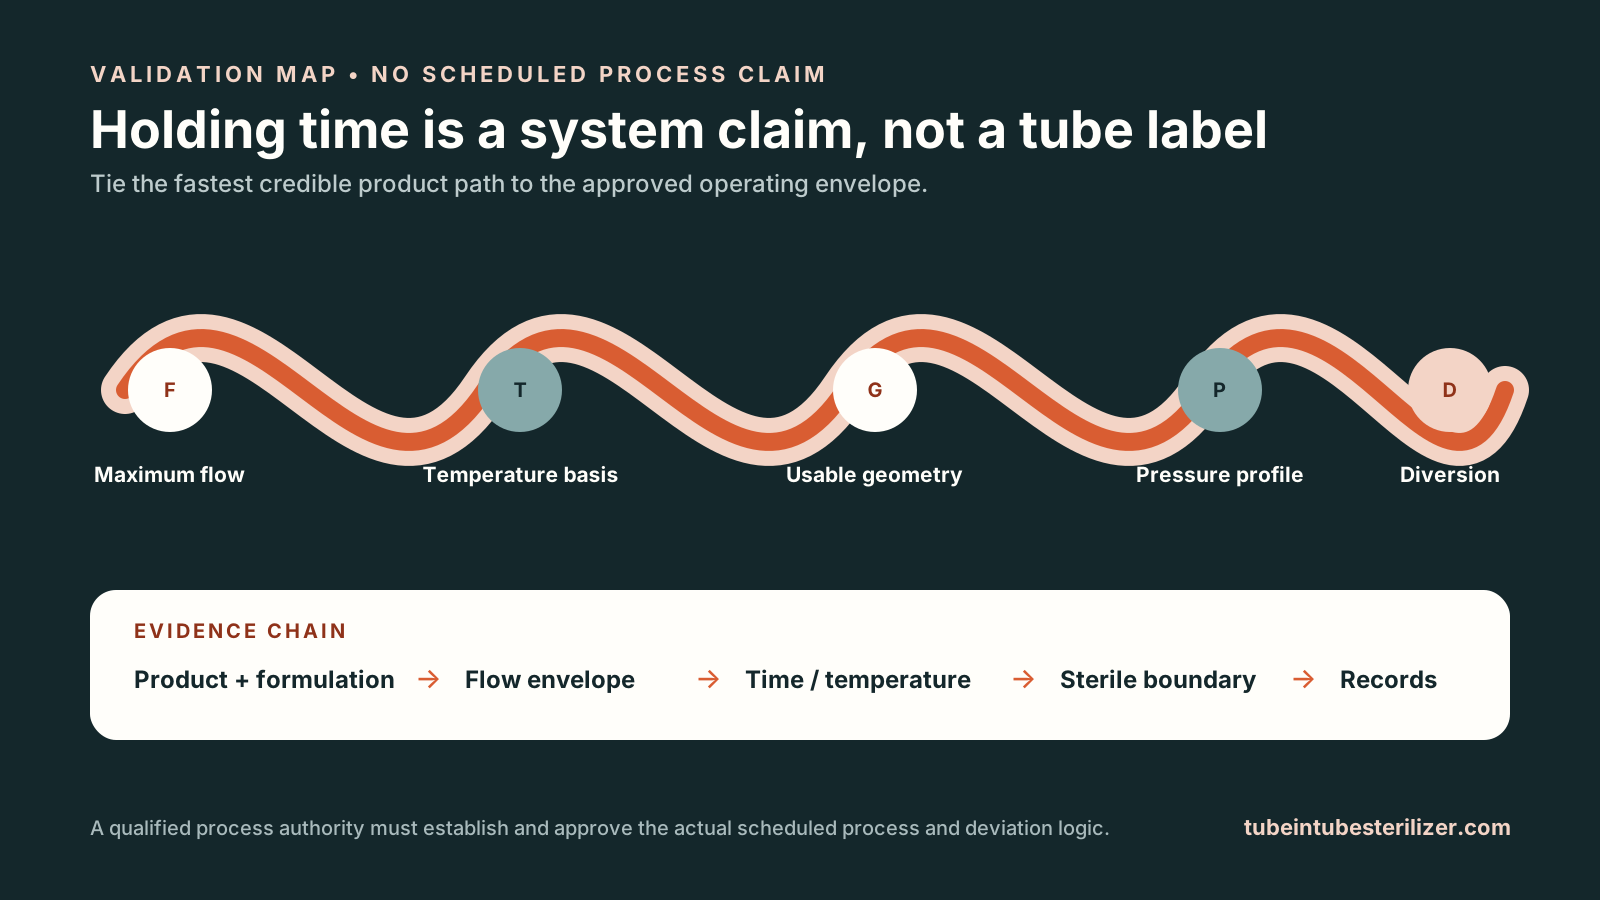
Food safety claims must be tied to the exact formulation, process, flow path, sterile zone, package and operating method. This page explains the planning boundary; it does not establish a scheduled process.
pH, water activity, formulation, viscosity, particles, heat penetration and target microorganisms influence the required process.
Holding geometry and the fastest product path must deliver the required minimum treatment under controlled flow.
The sterile zone includes the holding-tube outlet and downstream product-contact equipment through filling and packaging.
Critical temperatures, flow, pressure, valve state, alarms, deviations and corrective actions need an agreed record.
Scheduled process
Where regulation or product risk requires it, a qualified process authority establishes the scheduled process. Equipment suppliers and integrators translate that requirement into heating, holding, cooling and controls, but should not invent a universal time/temperature formula.
Changes to formulation, particle profile, flow, hold geometry, sterile-zone equipment, package or operating procedure may require reassessment.
Scope note: the FDA sources below address U.S. low-acid aseptic processing and filing. They are not a universal rule set for every product, market or thermal duty.
Control record
Reference instruments, recording devices, locations, accuracy checks and deviation limits.
Metering method, maximum permitted rate, pump/control relationship and holding basis.
Product/service pressure and any sterile/unsterile differential-pressure requirement.
Holding-section geometry, flow assumptions and the minimum treatment requirement.
Diversion, recirculation, sterile barrier and safe startup/shutdown sequence.
Package sterilization, filler condition, container integrity and storage basis.
Source library
These external sources describe general thermal-processing and hygienic-design principles. Their presence is not an endorsement, certification, or equipment-performance claim for Site34.
Claim boundary
Specific performance, material, certification, capacity and commercial claims remain pending until Site34-owned engineering evidence is reviewed.
Build the validation boundary early
A complete brief reduces late changes to holding, cooling, diversion and aseptic interfaces.
Request a quotation